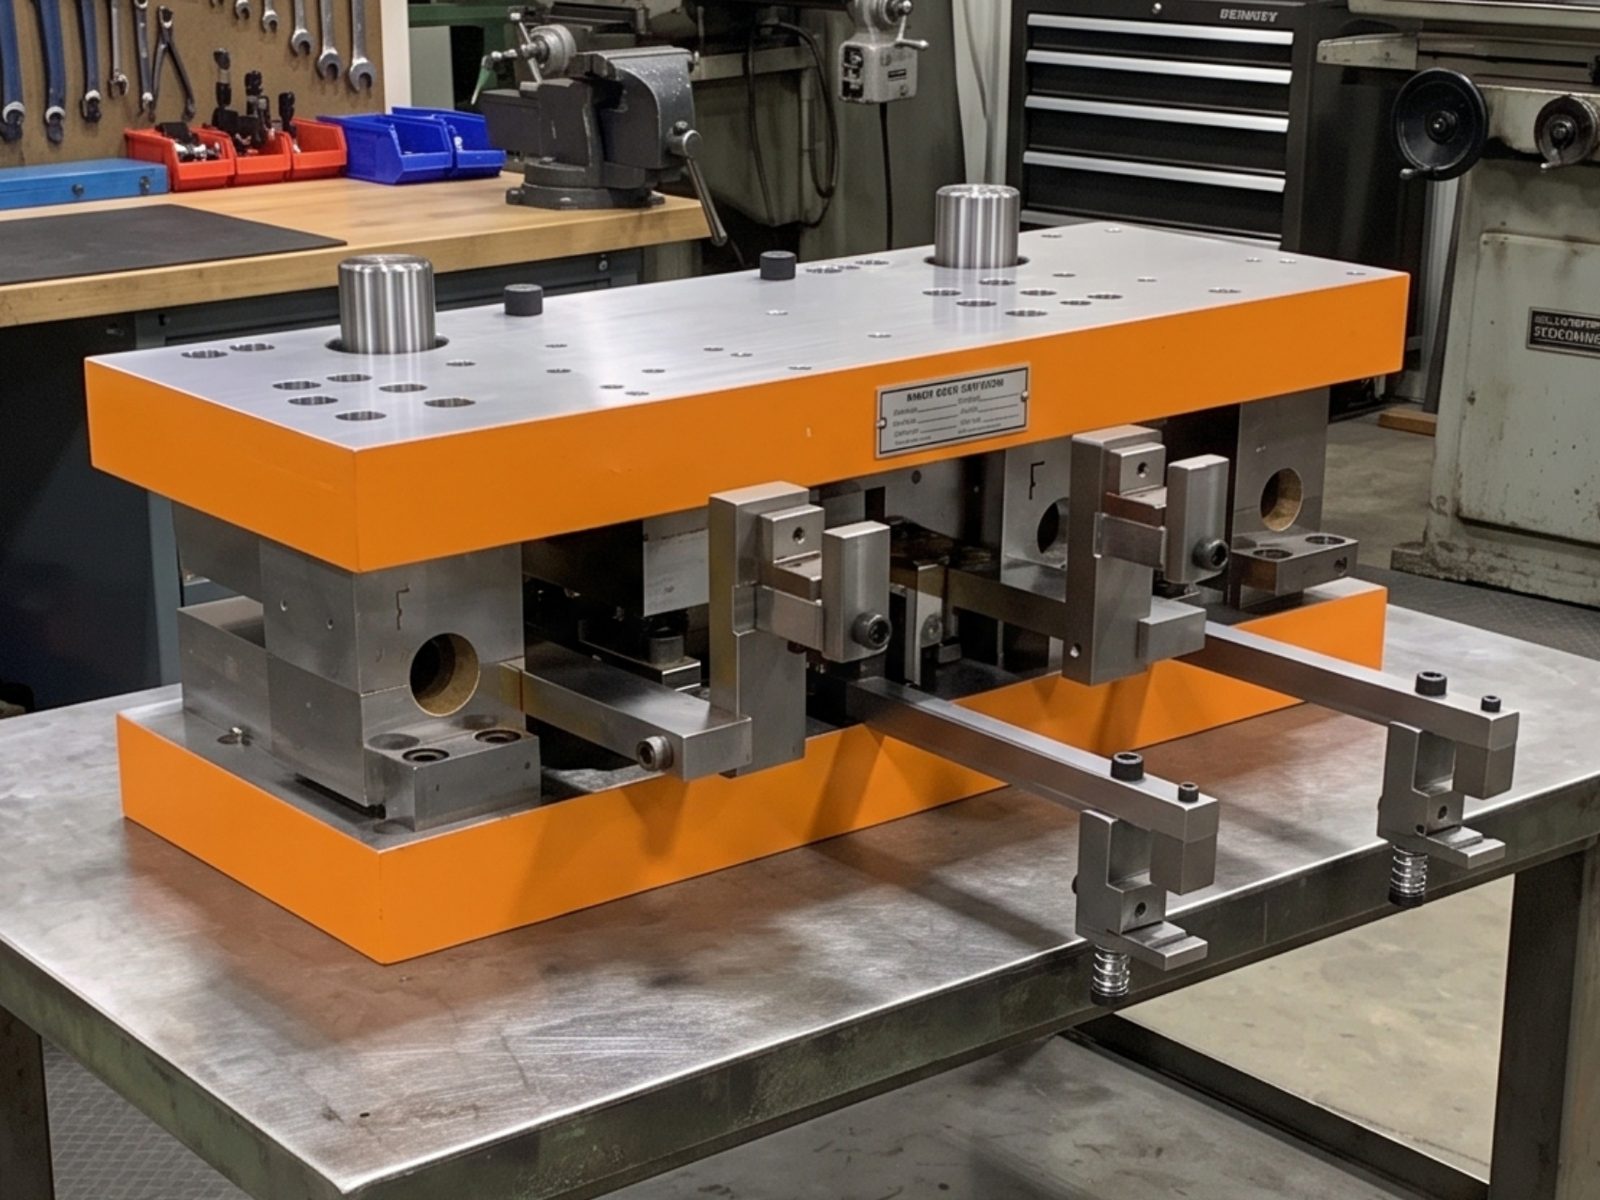
Custom dies for piercing, notching, coping, cut-off, and trimming tube, pipe, and extruded profiles — designed and built in Innovo's own tool and die shop since 1995. We also rebuild and retrofit dies built by other shops.
A custom die exists because no standard tool makes your part. Innovo designs and builds dies for one job: producing your part, at your rate, on the press or machine you already run. Because the same shop builds the machines those dies run in, the die and the process are engineered together rather than fitted to each other afterward.
Our tool and die work covers tube and pipe piercing, end notching and coping, cut-off and trimming, and forming — in round, square, rectangular, and extruded profiles. Every die is designed, machined, assembled, and tried out in-house in Elk Grove Village, Illinois.
Each die is sized to the part, the material, and the press or machine it will live in.
Single-hole and multi-station dies for holes, windows, and patterns in tube, pipe, and extrusions — including piercing over a mandrel for thin-wall sections.
End-notch and saddle dies that produce a clean, repeatable fit-up for welding, including the double-notch tooling used in Innovo's H237DN series.
Punch-press cut-off dies from 1" to 6" round capacity, and special dies for cutting and trimming bent tubular parts after bending.
Forming, flattening, and combination dies for parts that need more than one operation in a single hit.
Not every die that needs work was built here. Innovo rebuilds and retrofits dies originally built by other die shops — worn dies, dies whose builder is gone, and dies that need to run a new part size or a changed print. We evaluate the existing tool, tell you plainly whether a rebuild or a new die makes more sense, and quote both when the answer is close.
Four things let an Innovo engineer size the die and quote it accurately.
A print or a sample part. A photo and a sketch with dimensions is enough to start.
Tube OD and wall, or profile and gauge, and the material — steel, stainless, aluminum, or other.
What the die will run in: an Innovo machine, your punch press (tonnage, bed, shut height), or another builder's machine.
Parts per hour or per shift you need. Rate drives whether the die is manual, automatic, or belongs in a machine.
Send the print, the material, and the rate. An Innovo engineer will scope the die and quote it — and you approve finished parts before it ships.